

A patch panel job looks simple until you’re staring at 48 ports, a spool of Cat6, and no clear plan for which wires go where. This patch panel wiring guide walks through the exact steps to punch down cable correctly the first time, so you’re not chasing intermittent link lights or re-terminating jacks after a client walkthrough. Whether you’re wiring a small office closet or a full commercial rack, the process is the same, and getting it wrong costs you time and credibility on site.
If you came here for a wiring diagram and a straight answer on T568A versus T568B, you’ll get both. We cover tool prep, cable stripping, conductor order, punch-down technique, and the testing steps that confirm every run before you close the rack. No fluff, just the sequence a working technician actually follows.
We put this guide together from what shows up on real service tickets, the punch-down mistakes that cause callbacks and the shortcuts that hold up under inspection. Mega Services staffs certified low-voltage and structured cabling technicians on jobs across the US and Canada, and clean terminations are non-negotiable for every one of them. Use this as your step-by-step reference next time you’re wiring a panel, or as a benchmark for what proper work should look like.
What you need before wiring a patch panel
Before you touch a single cable, get your gear staged. Running back to the truck mid-job because you forgot a punch-down tool is how a two-hour job turns into a four-hour job, and it’s the kind of thing that makes a client question whether you know what you’re doing. Gather everything first, check it against a list, and you’ll move through the panel without interruption.
Tools you actually need
You don’t need a truck full of gear for this. A patch panel wiring job comes down to a short list of tools, but skipping any one of them will slow you down or hurt the quality of your terminations.
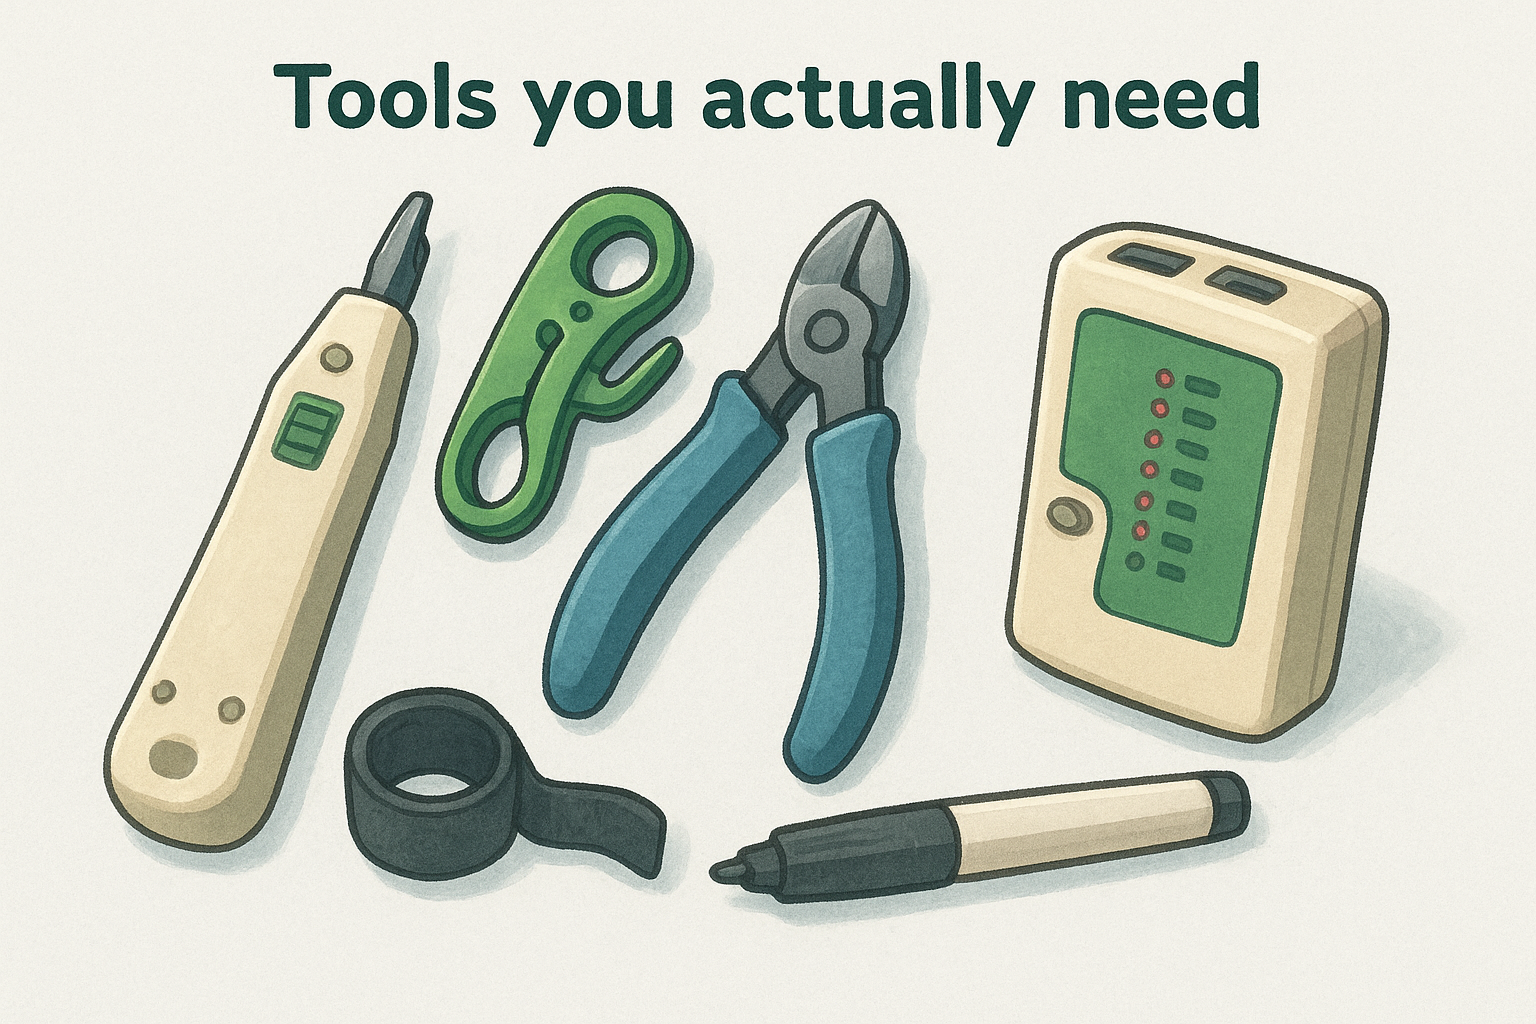
- Punch-down tool with a 110 blade (get one with an impact adjustment so you’re not overdriving or underdriving contacts)
- Cable stripper rated for the jacket diameter you’re working with, a standard coax/twisted-pair stripper works for most Cat5e/Cat6 jobs
- Diagonal cutters or scissors for trimming conductors flush after punch-down
- Cable tester (a basic continuity tester works, but a certifier is better if you’re billing the job as certified)
- Velcro cable ties or hook-and-loop wraps, never zip ties on data cable, they crush the jacket and change the cable’s electrical characteristics
- Labels and a label printer or permanent marker for port and cable ID
- Flashlight or headlamp, most racks sit in closets with bad lighting
A punch-down tool with the wrong blade or a stripper that nicks conductors will cause more failed terminations than any wiring mistake you make later.
Materials to have on hand
Beyond tools, you need the right consumables staged before you start pulling cable through the panel. Running short on patch panels or labels mid-install means a second trip, and on a commercial job that second trip comes out of your margin.
| Material | What to check |
|---|---|
| Patch panel | Port count matches your cable run count, with a few spares for future drops |
| Cat5e/Cat6/Cat6a cable | Matches spec called for in the project scope, don’t mix categories on the same run |
| Cable management bars or D-rings | Enough to support the full bundle weight without sagging |
| Rack screws or cage nuts | Sized to the rack you’re mounting into |
| Labels | Both ends of every cable, plus the panel port itself |
Know your wiring standard before you start
Decide on T568A or T568B before you strip a single cable, and confirm it against the existing infrastructure if you’re extending someone else’s network. Mixing standards mid-project is one of the most common causes of crossed pairs and dead ports, and it’s an easy mistake to make when you’re moving fast across a big rack. Most commercial installs in the US default to T568B, but always check the job spec or existing panel labeling before assuming.
Read the cable run list and the rack elevation
Grab the cable schedule or run list before you plug in the punch-down tool. Knowing which cable lands on which port, and in what order the ports are supposed to fill, keeps your documentation matching reality once the job closes out. If there’s no run list, build one on the spot, a five-minute spreadsheet now saves an hour of tracing cable later.
Confirm your workspace and access
Lastly, check that you’ve actually got room to work. A crowded rack with cables from three other trades tangled through it makes clean punch-downs almost impossible, and it’s worth five minutes to clear a path before you start. Confirm power and lighting at the rack location too, since closets and server rooms often run on a single dim fixture that won’t show you a badly seated conductor until it’s too late.
Project managers coordinating multi-site rollouts often find this staging step is where jobs go sideways, not the actual wiring. If your team is running structured cabling across several locations at once, Mega Services can supply certified technicians who show up with the right tools and the run list already in hand, so the staging step isn’t left to chance.
Step 1. Map and label your cable runs
Before you punch down a single wire, walk the run and confirm where each cable actually starts and ends. Mapping the cable run means physically tracing or verifying every cable from its origin (a wall jack, camera, or access point) to its destination at the patch panel, not just trusting whatever label the last person left on it. Mislabeled runs are one of the top causes of callback tickets, and they’re almost always avoidable with ten extra minutes of tracing before termination.
Build a simple labeling scheme
Use a consistent numbering system across the whole job, not one you’re inventing port by port as you go. A common approach ties the label to the physical location and drop number, something like this:
Floor-Room-DropNumber
Example: 2F-CONF3-04
(2nd floor, Conference Room 3, drop 4)
Write that same identifier on both ends of the cable and on the corresponding panel port. Consistent labeling across the whole rack means anyone who opens that panel in six months, whether it’s you or a different technician, can trace a run without pulling cable through the wall to check it.
Use a tone generator if the far end isn’t obvious
If you’re working a retrofit or a rack someone else started, don’t guess which cable goes where. Clip a tone generator to the far end, walk the panel with the inductive probe, and confirm the match before you commit it to a labeled port. This takes two minutes per run and eliminates the guesswork that leads to swapped ports on the documentation later.
A mislabeled cable is worse than an unlabeled one, because it sends the next technician chasing the wrong problem entirely.
Update the run list as you go
Keep the cable schedule open next to you, whether it’s a printed sheet or a spreadsheet on a tablet, and check off each run as you confirm and label it. Fill in gaps immediately rather than trying to reconstruct the list from memory at the end of the job. Real-time documentation during the mapping step is what makes closeout fast instead of painful, and it’s the difference between handing a client a clean as-built and spending an extra hour reverse-engineering your own work.
Once every run is traced, labeled, and logged against the schedule, you’re ready to move to the panel itself. Skipping this step to save time up front almost always costs more time later, usually while a client is standing behind you asking why port 14 doesn’t match the drawing.
Step 2. Strip the cable jacket
Once a run is mapped and labeled, cut it to length with a few inches of slack at the panel and strip the jacket back far enough to work with, but no further than you need. Stripping too much jacket exposes the twisted pairs to interference and gives you loose conductors that are harder to seat cleanly, while stripping too little leaves you fighting the punch-down tool. Most patch panels are built for about half an inch to one inch of exposed conductor, so check the panel manufacturer’s spec before you start cutting jacket on every run.
Set the stripper and make the cut
A cable stripper with an adjustable blade depth is worth the extra ten dollars over a fixed blade, because Cat5e and Cat6 jackets vary in thickness and a blade set too deep will nick the copper inside. Score the jacket, don’t try to cut all the way through in one pass, then twist the stripper around the cable and pull toward the end to slide the jacket off.
Strip length reference:
T568A/T568B panel termination: 0.5" - 1" exposed conductor
Keystone jack termination: match panel spec, usually similar range
Do not strip more than needed to reach the punch-down block
A nicked conductor under the jacket won’t show up until the cable fails a certification test, and by then the jacket’s already closed back over it.
Check for nicks before you move on
Run your fingers along the exposed conductors after stripping and look closely under good light, since a nicked wire can pass a quick continuity test now and fail intermittently later once the rack gets bumped or a tech leans on the bundle. Checking for nicks takes five seconds per cable and it’s the cheapest insurance you’ll buy on the whole job. If you find a nick, cut the cable back past it and strip again rather than hoping it holds.
Keep the twist intact until punch-down
Don’t untwist the pairs any further than necessary while you’re stripping, and don’t let them sit untwisted for more than an inch or two before they land in the punch-down block. Cat6 and Cat6a in particular rely on tight, consistent twist rates to maintain their crosstalk performance, and pulling pairs apart early undoes some of that engineering before the cable’s even terminated. Keep the bundle tight, keep the jacket cut clean, and move straight into arranging the wires once you’ve confirmed there’s no damage underneath.
Step 3. Arrange the wires to T568A or T568B
With the jacket stripped and the pairs intact, untwist just enough conductor to fan the wires flat in the correct order. Arranging the wires correctly before punch-down matters more than the punch-down itself, because a wire in the wrong slot will pass a quick plug test but fail a certifier or cause random dropouts once the switch is under load. Match the standard you settled on during staging, and don’t switch mid-panel just because one run feels easier to arrange the other way.
Know the pin order for both standards
T568A and T568B use the same eight positions on a punch-down block, but pairs 2 and 3 swap places between the two standards. Here’s the reference to keep next to the panel:
| Pin | T568A | T568B |
|---|---|---|
| 1 | White/Green | White/Orange |
| 2 | Green | Orange |
| 3 | White/Orange | White/Green |
| 4 | Blue | Blue |
| 5 | White/Blue | White/Blue |
| 6 | Orange | Green |
| 7 | White/Brown | White/Brown |
| 8 | Brown | Brown |
Get pins 2 and 3 backwards and the cable will still pass a basic continuity test, right up until it fails under real network load.
Fan the pairs without over-untwisting
Separate the four pairs first, then untwist each individual pair only as far as needed to lay the two conductors flat against the color-coded slots on the panel’s 110 block. Fanning the pairs this way keeps most of the twist intact right up to the termination point, which matters for Cat6 and Cat6a performance under Ethernet’s higher data rates. If a conductor keeps springing back out of position, you’ve likely untwisted more than necessary, so tighten it back up and try again.
Match the color code printed on the panel
Every patch panel has the color code printed right on the housing, usually with both A and B options labeled next to each slot. Read it before you lay in a single wire, since panels from different manufacturers sometimes print the label at a slightly different angle or spacing than you’re used to. Confirm the printed code matches the standard on your job spec, then lay each conductor into its slot in order, working left to right across the eight positions so you’re not doubling back and re-checking wires you already placed.
Once all eight conductors sit in their correct slots and the twist looks even across the fan, you’re ready to seat them with the punch-down tool.
Step 4. Punch down the wires into the panel
With every conductor fanned into its slot, seat the punch-down tool over the first wire and press straight down until it clicks. Punching down the wires is the step that actually makes electrical contact, so a sloppy angle or a rushed strike here undoes all the careful arranging you just did in Step 3. Work one pin at a time, confirm the wire is fully seated in its slot before you strike, and don’t let the tool drift off-axis or you’ll bend the contact instead of seating it cleanly.
Orient the blade correctly
Most 110 punch-down tools have a cutting side and a non-cutting side, and mixing them up either leaves excess wire hanging or trims the conductor you meant to keep. Point the cutting edge toward the outside of the panel so the blade trims the tail of the wire, not the piece that carries signal back into the block. Check your tool’s manual once if you’re not sure, since a backwards blade on a brand-new hire’s first panel is a common enough mistake that it’s worth the thirty seconds to confirm.
Seat every conductor with the same pressure and angle, because an inconsistent punch-down is where intermittent faults come from months later, not day one.
Work the pins in a consistent order
Go left to right across the eight positions instead of jumping around the block. Working in order keeps you from losing track of which wire you’ve already seated, especially on a long run of ports where every panel looks identical after the tenth one. If you get interrupted mid-panel, this order makes it easy to pick back up without second-guessing yourself.
Trim and inspect each connection
After the tool clicks, check that the excess conductor sheared off flush with the block and didn’t leave a stray wisp that could short against the next pin. Run a finger lightly across the row once you’ve punched all eight positions, feeling for anything sitting too high or an obviously loose contact. Inspecting each connection before moving to the next port catches a bad seat while it’s still a thirty-second fix, instead of a callback after the rack’s closed up and labeled.
Confirm the pair count before closing the port
Double-check that all four pairs, all eight wires, actually made it into the block. It sounds obvious, but a pair that slipped out while you were fanning wires in Step 3 is easy to miss until you’re staring at a failed test result later. Count the wires against the diagram one more time before you move to the next port on the panel.
Step 5. Dress and secure the cable bundle
Once every port on this row is punched and inspected, turn your attention to the cable behind the panel before it turns into a tangled mess. Dressing the bundle means routing each cable neatly to a management bar or D-ring, grouping runs logically, and securing them without crushing the jacket or straining the termination you just made. Skip this step and you’re left with a rat’s nest that makes future troubleshooting slow and turns a clean install into something a client notices for the wrong reasons.
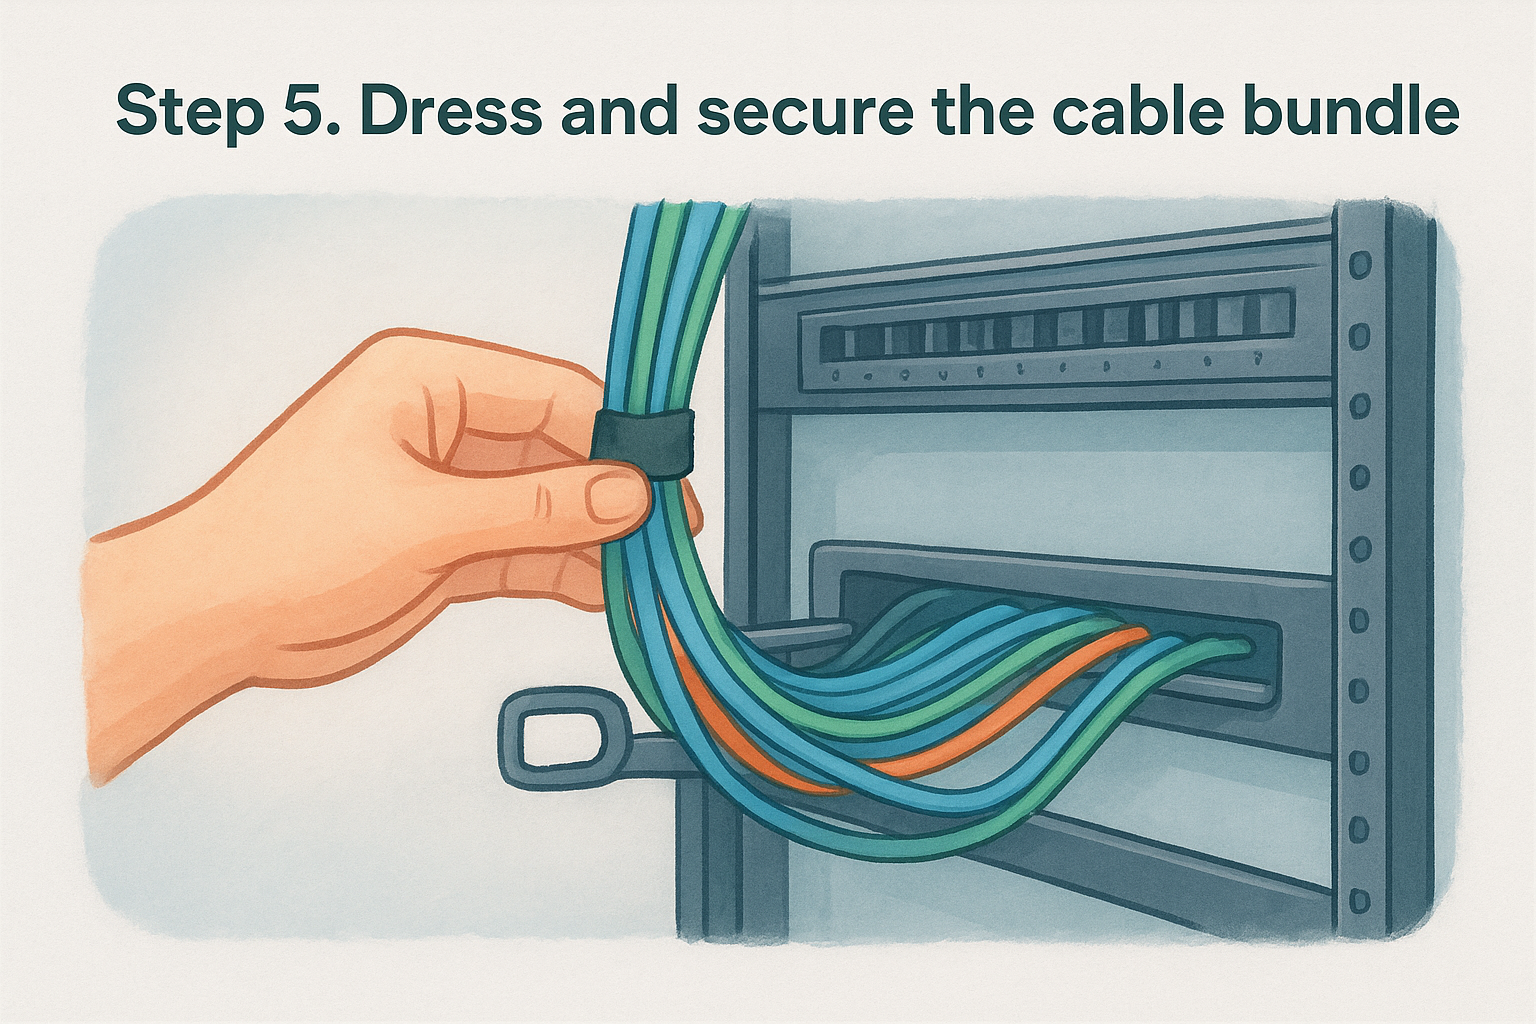
Route to the management bar first
Gather the cables coming off the back of the panel and route them down to the horizontal management bar or D-rings mounted below or beside the rack section, rather than letting them hang loose off the punch-down block. Routing to the management bar takes the physical weight and pull off the termination point itself, so a tech leaning into the rack next month doesn’t yank a wire loose. Keep runs going to the same port group bundled together, since that makes tracing a single cable later far faster than digging through a mixed bundle.
Tie loosely, never tight
Secure the bundle with hook-and-loop wraps at consistent intervals, snug enough to hold the shape but loose enough that you can slide a finger under the tie without effort.
- Space ties every 12 to 18 inches along a vertical run
- Never cinch a tie so tight it dents the jacket
- Alternate tie tension across the bundle so no single cable bears all the pressure
- Skip zip ties entirely on data cable, hook-and-loop only
A cable tie cinched too tight does the same damage as a stripper blade set too deep, it just takes longer to show up as a failed test.
Preserve bend radius and leave slack
Check that no cable bends sharper than roughly four times its own diameter, since a tight bend pinches the pairs inside and degrades performance in a way that won’t always show on a basic continuity check. Preserving bend radius matters more at the panel and at any 90-degree turn in the rack than anywhere else in the run, because that’s where techs are most likely to force a cable into a tight corner to make the row look neat. Leave a small service loop, an extra six to twelve inches, coiled behind the panel so a future re-termination doesn’t require pulling slack from somewhere down the run.
With the bundle dressed, tied, and routed clear of sharp bends, you’re ready to confirm the work actually performs the way it looks.
Step 6. Test your connections and troubleshoot
With every port punched, dressed, and labeled, plug in the tester and confirm each run actually works before you call the job done. Testing your connections is the step that catches the mistakes hiding under Steps 3 and 4, a swapped pair or a nicked conductor that looked fine to the eye but fails the moment current runs through it. Never skip this because the panel looks clean, a good-looking termination and a working one are not the same thing.
Run a continuity test on every port
Start with a basic continuity or wiremap test on each run, checking that all eight pins map correctly from patch panel to the far-end jack or plug. Most inexpensive testers will flag an open, a short, or a reversed pair within a few seconds per port, and running through the whole panel this way rarely takes more than fifteen minutes on a standard 24-port row.
A basic wiremap test catches most termination mistakes in under ten seconds, and there’s no excuse for skipping it on a single port.
Certify the link if the spec requires it
If the job scope calls for certified Cat6 or Cat6a performance, a basic continuity tester won’t cut it. Certifying the link means running a proper certifier that measures attenuation, crosstalk, and return loss against the category standard, not just confirming the wires connect. The TIA/EIA 568 standard defines the performance thresholds a certifier checks against, and clients paying for certified cabling expect a printed report showing every run passed.
Troubleshoot common failures
When a port fails, work through the likely causes in order rather than re-punching blind. Most failures trace back to one of a handful of repeat offenders:
| Symptom | Likely cause | Fix |
|---|---|---|
| Open pin | Wire not seated, missed slot | Re-punch that pin only |
| Split pair | Wrong conductor in slot 3 or 6 | Re-check T568A/B order |
| High crosstalk | Over-untwisted pair, tight bend | Re-terminate, fix bend radius |
| Intermittent link | Nicked conductor, loose tie | Cut back and re-strip |
| No continuity at all | Wrong far-end jack, mislabeled run | Re-trace with tone generator |
Log the results before closing the rack
Save or print the test results for every port, whether it’s a basic pass/fail list or a full certification report, and attach it to the job documentation you hand the client. Logging the results now means nobody has to re-test a working port six months from now just to prove it was done right, and it’s the paperwork that protects you if a dispute ever comes up about whether the cabling was installed to spec.
Keeping your patch panel running smoothly
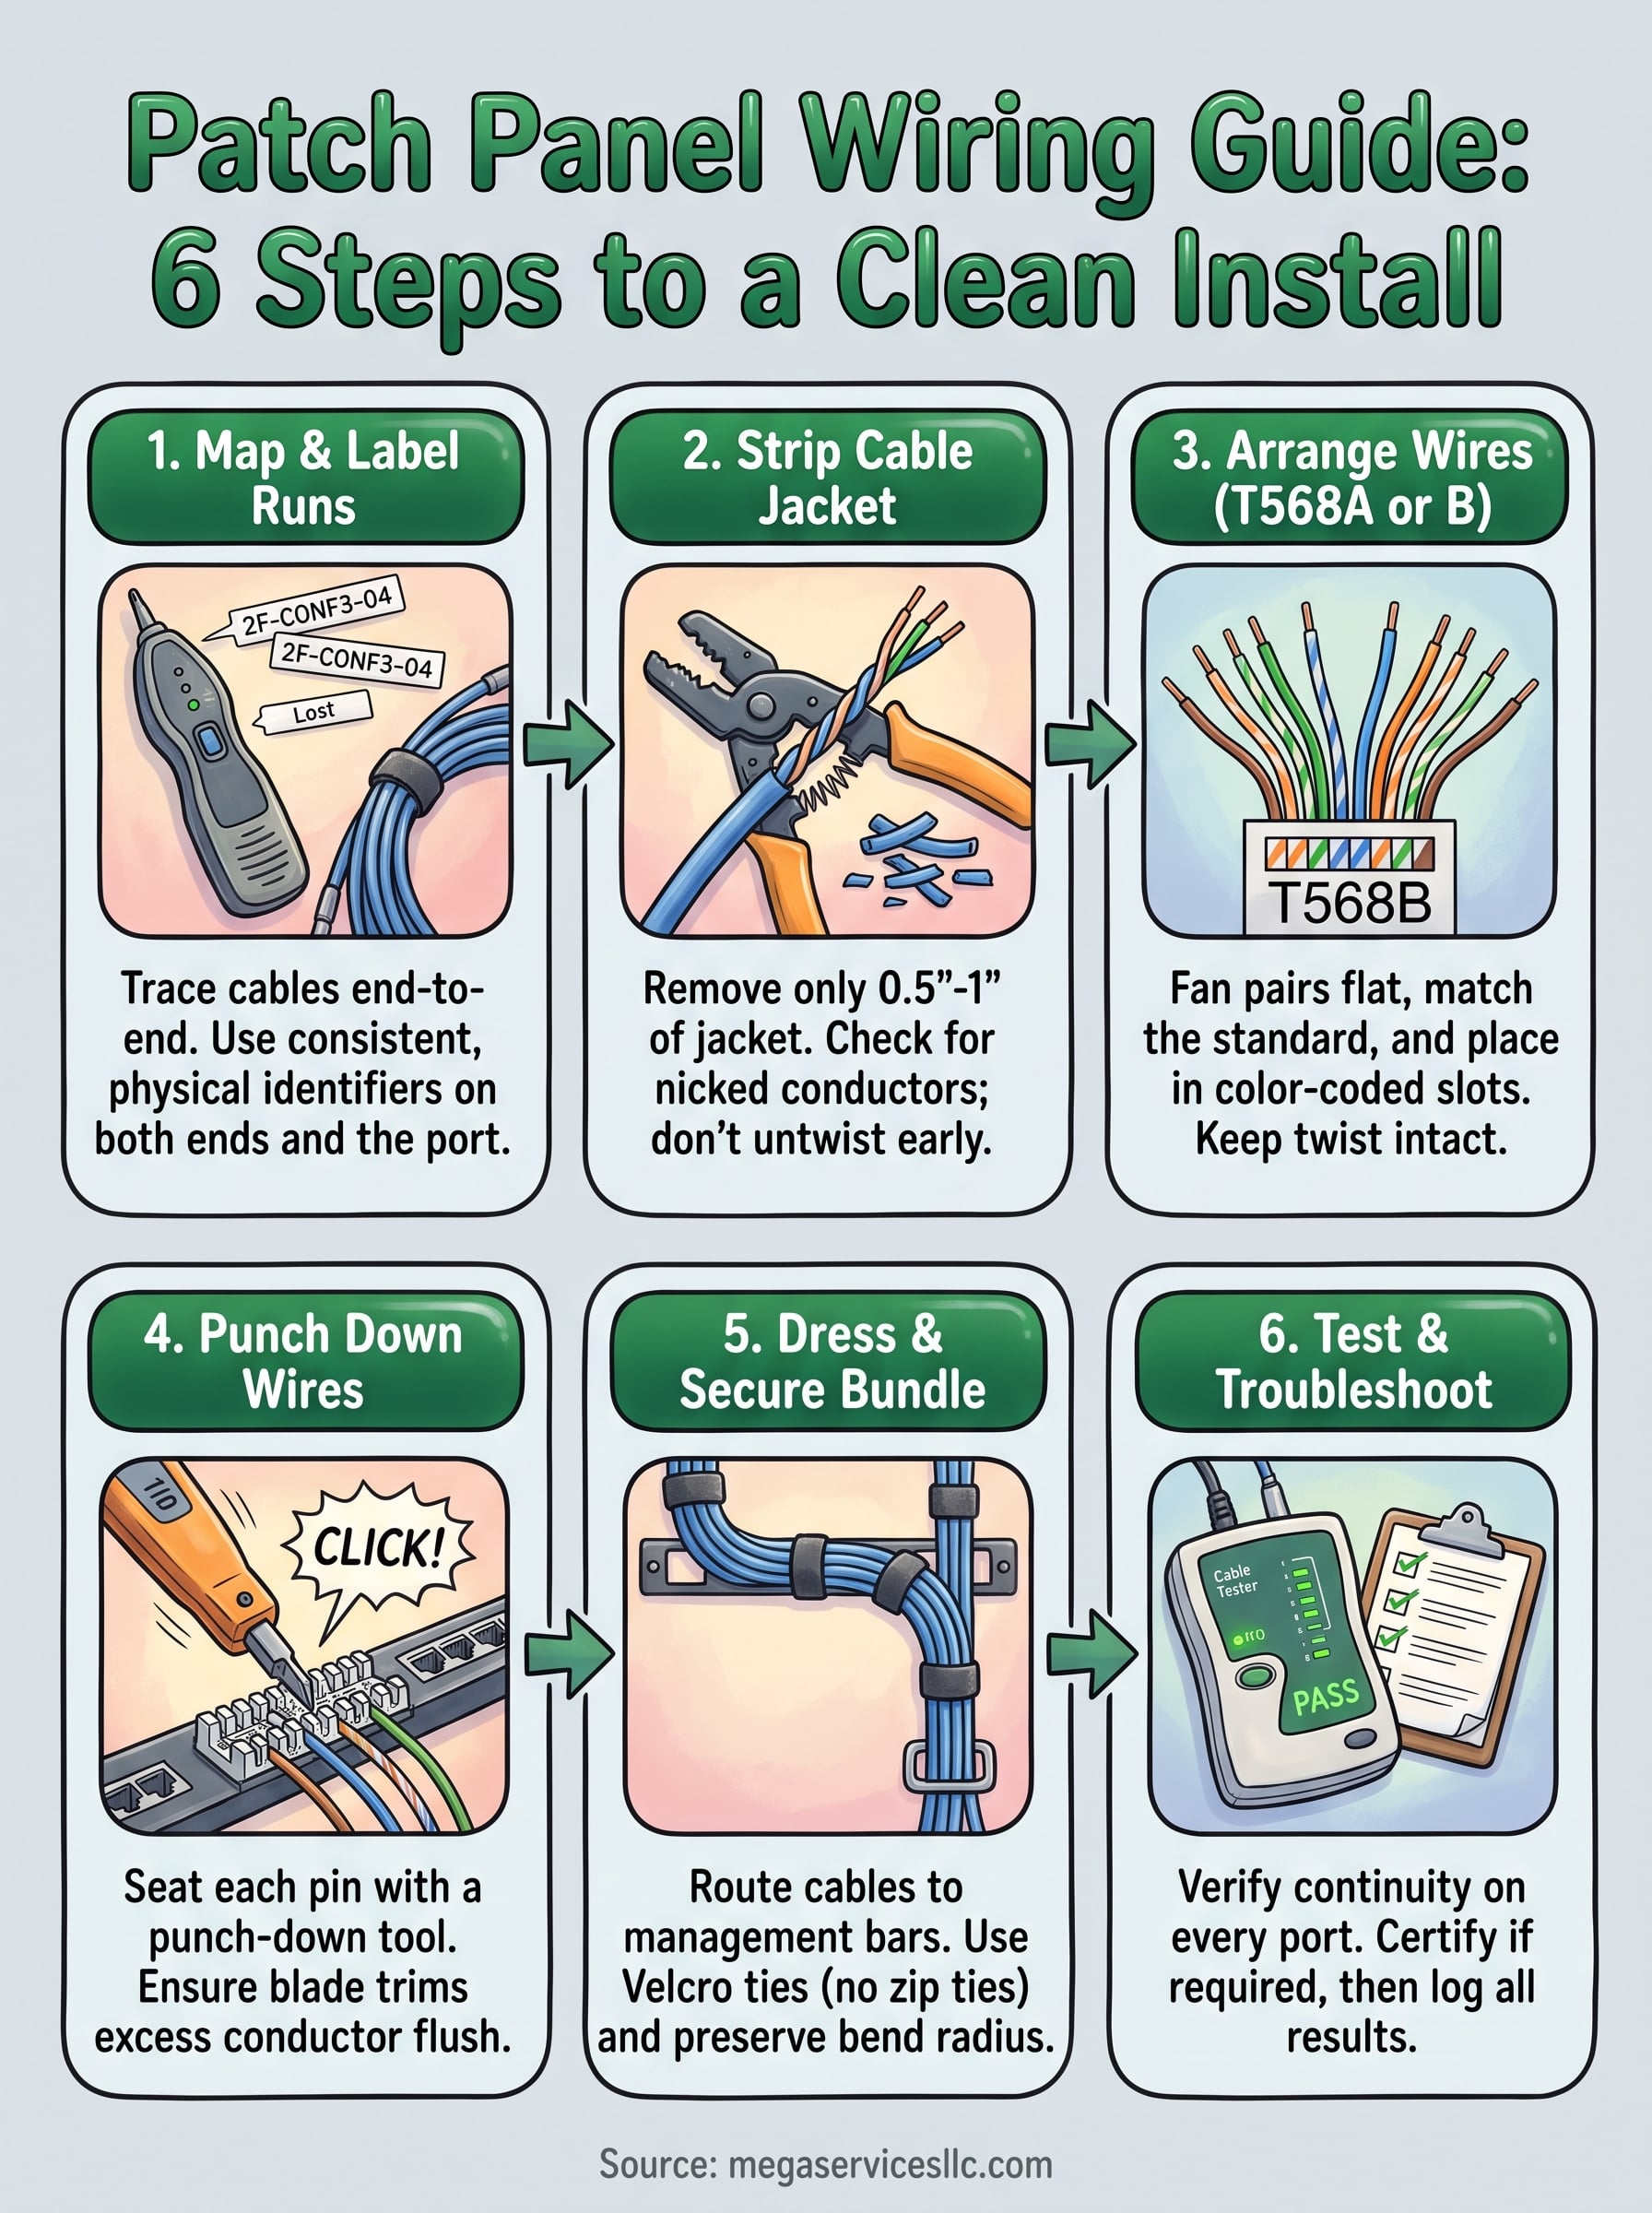
A patch panel wired right the first time doesn’t need much attention after closeout. Consistent standards, clean punch-downs, and dressed bundles hold up for years, while shortcuts on any of the six steps above tend to surface as callbacks within the first few months. Revisit your labeling and test logs any time you add drops to the rack, and keep the same T568A or T568B standard across every future run so nobody inherits a mismatched panel down the line.
Most jobs go sideways from rushed staging or skipped testing, not from a lack of skill on the tools. If you’re managing rollouts across multiple sites and need technicians who show up with a run list, a certifier, and the discipline to test every port before they leave, book a MegaTech for your next project and get the certainty a clean rack actually requires.
Mega Has The Staffing Solutions You Need For Your Next Pro AV Project.
Let MegaServices help you grow your business by providing you with the qualified personnel you need when you need them.
Allie Linarez is a Senior Billing Specialist at MegaServices LLC. As one of Mega’s earliest team members, Allie has grown with the company and contributed to many of the processes used today. Her adaptability, organization, and attention to detail make her a trusted part of Mega’s service-side billing operations.
